Filling and Sealing Machine Solutions: A Practical Guide to Smarter Packaging Lines
2026-11-16
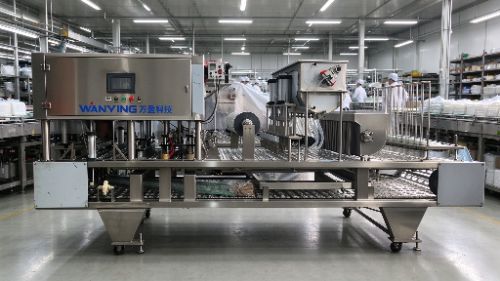
Packaging lines rarely fail all at once. They slow down first: a seal drifts out of tolerance, a fill level begins to waver, and suddenly a line that once ran smoothly is chewing through film and losing product. At Wanying Machinery, we see this pattern constantly, and the fix is rarely another patch or a faster operator. It is a smarter approach to filler-sealer integration. This guide breaks down practical solutions for tightening fill accuracy, improving seal consistency, and reducing the small inefficiencies that quietly drain output. If your line feels like it is working against you rather than with you, the next few sections will show you where to look first and what to change for lasting results. More details on our equipment approach can be found at Wanying Machinery.
Filling Methods That Match Product Behavior
Matching a filler to the way a product moves often matters more than a single viscosity reading. Chunky sauces can bridge in a gravity-fed hopper, while airy foams collapse under aggressive agitation. Running small batches through candidate nozzles and observing how the material settles, strings, or splashes gives you a practical read that datasheets rarely capture.
Carbonated beverages call for counterpressure filling to keep dissolved gas from breaking out, while hot-filled jams and syrups lean on temperature to stay fluid long enough to seal cleanly. Shear-sensitive creams and particulate soups often respond better to rotary or progressive cavity pumps than to high-speed piston strokes. The aim is to preserve texture and suspension instead of forcing every product through the same motion.
Filling method also affects portioning logic. Thin, stable liquids suit volumetric nozzles, but products with variable chunk size or high value usually justify net-weight or weigh-cell feedback to avoid giveaway and short fills. Watching how a product drips, de-aerates, or clings to a nozzle can guide details like cut-off design, drip trays, and container positioning that make the line run with fewer interruptions.
Sealing Decisions Under Production Pressure
Field crews rarely get the luxury of ideal conditions when a seal starts weeping under load. The decision usually comes down to what is on the truck, how long the well can stay offline, and whether the last replacement actually held. That last detail matters more than most manuals admit. A seal that failed early often leaves behind clues such as uneven compression, localized extrusion, or a polished bore with faint scoring. Those signs should redirect the next choice instead of simply repeating the same part number.
There is a common reflex to treat sealing problems as one-size-fits-all once production targets are looming. Teams grab the same elastomer or metal-to-metal setup that worked on a nearby well and call it good. But thermal cycling, solids in the flowstream, and slight misalignment can turn an acceptable seal into a slow leak within weeks. Reading the removed hardware, checking flange face flatness, and recording exact make-up torque give far better guidance than relying on a generic spec sheet.
The hardest calls happen when a seal is holding but clearly near its limit. Replacing it means deferring output and possibly triggering a full shutdown review. Pushing it further risks a weekend failure with worse consequences. Experienced supervisors often set a clear tripwire such as an observed pressure drop, a visible bubble test result, or a change in bolt load before the pressure to keep producing overrides judgment. That way the decision is made before the pressure peaks, not during it.
Changeover Sequences Worth Standardizing
Some changeovers eat hours because people re-derive the same order every time, not because the tasks themselves are difficult. The sequences worth capturing often look obvious only after someone finishes them. A die change that needs four trips to the tool crib, a packaging line switch where labels get checked too late, or a mixer cleanup that keeps alternating between wet and dry steps is a solid candidate. Recording the actual order of these moves, including small backtracking moments, usually shows where time is leaking.
Frequency matters less than the gap between operators or shifts. If two experienced people prepare the same machine and one routinely finishes twenty minutes earlier, that difference is worth studying. Standardizing the sequence means writing down the small decisions: where parts are staged before shutdown, when maintenance gets called, which bolts are loosened before power is cut. The goal is not to impose one rigid method but to make the better choices visible enough to copy.
A workable standard tends to be a short list kept at the workstation, arranged in the order work actually happens rather than as a polished training outline. It can leave room for minor habits, such as which hand adjusts a guard or who carries the next batch of inserts, while fixing the steps that affect safety, quality, and setup time. When the sequence is specific enough to guide a new operator and loose enough that an experienced one will not ignore it, it has earned its place.
Inline Inspection Without Bottlenecking
A lot of inline inspection gets blamed for slowing down a line when the real issue is latency in the capture chain, not the camera itself. The moment a part must pause, wait for a trigger, or sit under a light long enough to avoid motion blur, throughput already starts leaking. Keeping the line moving means treating image acquisition as a synchronous event tied to encoder position rather than a separate station with its own clock.
Lighting and processing have to be designed around the fastest product you expect to run, not the average. Short exposure times freeze motion without needing the conveyor to stop, but they demand more light intensity and cleaner signal. That tradeoff is manageable when the inspection algorithm runs on dedicated hardware or a tightly optimized edge device, so decisions arrive in the same beat as the next part.
Reject handling matters just as much as image capture. A slow diverter or a delayed signal can back up good product behind a single bad unit. Pushing the pass/fail decision closer to the point of ejection, usually within a few milliseconds, lets the line keep its cadence while still removing defects cleanly. When timing is right, inspection stops being an interruption and becomes part of the machine's own rhythm.
Sanitary Design Beyond the Checklist
Sanitary design often gets reduced to a pass/fail exercise: sloped surfaces, continuous welds, no exposed threads. But the checklist only captures what was already known to be a problem. The more useful work happens when you ask where water actually sits after a washdown, how far spray can travel behind a bracket, or whether an operator can see the area they're expected to clean. Those questions reveal gaps that a standard audit rarely records.
Designing beyond the checklist means treating cleanability as a property of the whole layout, not a collection of approved parts. A tank can meet every surface finish spec and still create a dead zone behind its support legs. A drain can have the right slope and still let aerosol drift back onto product zones. The difference shows up in details that resist the usual categories: shadowed corners, overlapping materials, joints that look tight at eye level but open under thermal movement.
The strongest plants treat the checklist as a floor rather than a ceiling. They keep updating it when new contamination patterns emerge, when a change to one line alters airflow, or when a cleaner finds a spot that takes twice as long as it should. That kind of attention doesn't produce a perfect score sheet. It produces a facility where sanitation becomes easier to execute, verify, and maintain with fewer hidden risks.
Line Layouts That Cut Walking and Waiting
Straight-line layouts often look tidy on paper, but they quietly multiply the distance people and parts travel. When a workstation is placed at the far end of a long row just to keep the line visually straight, every material replenishment, quality check, and tool swap becomes a round trip. Bending the flow into a U-shape or grouping machines by product family brings the start and end of a sequence closer together, so one operator can watch several steps without walking half the building.
The payoff shows up most in the gaps between operations. If a part sits on a rack waiting for someone to walk it to the next station, the layout is creating idle time that no amount of overtime can fix. Tighter cell designs shorten those handoffs to a few steps, and visual buffers placed between stations let people see when to feed or slow down before a bottleneck forms.
A useful test is to map a single order through the floor and circle every movement that is not actually changing the product. The circled path usually looks like a knot. Straightening that knot rarely means expensive automation; it means moving benches, racks, and inspection points close enough that walking and waiting stop being accepted as part of the job.
FAQ
Viscosity changes everything from nozzle design to pump choice. Thin, watery products often do well with gravity or overflow fillers, while thick pastes and gels need positive displacement pumps and heated hoppers. Ask suppliers to run trials with your actual product, not just a close substitute, because small differences in solids content or temperature can shift fill accuracy noticeably.
Format changes often disturb sealing temperature, dwell time, and pressure in ways operators don't immediately see. The sealing heads or jaws may need recalibration for new cup or tray dimensions. Keeping a record of validated settings per format saves time and reduces the temptation to just tweak a dial mid-shift.
Integrated machines reduce transfer points and make it easier to hold a clean, controlled environment, but a separate filler and sealer can offer more flexibility when product ranges change often. If floor space is tight and formats are fairly stable, a monobloc system usually pays off. For high-mix operations, separate units with smart conveyors give more room to rearrange.
Look at where operators lose minutes: searching for parts, manual adjustments without reference marks, and cleaning procedures that require full disassembly. Simplifying tool-free parts, using quick-release clamps, adding digital recipe storage, and staging change parts near the machine can often trim changeover by thirty to fifty percent with minimal capital.
Temperature affects both product flow and seal quality. A product that thickens as it cools may need jacketed hoppers or heated nozzles. On the sealing side, too much heat can melt thin films or distort containers, while too little creates weak seals. Closed-loop temperature control with feedback keeps conditions stable during long runs.
Giveaway often comes from running a safety margin that's wider than necessary. Checking fill weight data over a full shift can reveal patterns tied to pump wear, temperature drift, or operator adjustments. Servo-driven pumps and in-line checkweighers with feedback help tighten tolerances, but even basic calibration routines and nozzle maintenance can recover a surprising amount of product.
Focus on the parts that wear in predictable ways: seals, O-rings, filling nozzles, sealing jaws, and film feed rollers. Instead of a generic checklist, use run-hour data or cycle counts to replace parts before they drift out of spec. Short daily inspections at shift handover catch leaks and misalignments while they're still cheap to fix.
Surfaces that slope to drain, minimal crevices, easy guard removal, and washdown-rated components matter as much as the control system. Look for designs that expose product contact areas without tools and avoid cable runs or brackets above open product. If you use wet cleaning, make sure the sensors and drives are genuinely rated for that environment rather than simply covered.
Conclusion
Filling equipment rarely fails because a pump is undersized; it fails when the machine treats a shear-sensitive emulsion like a thin water-like fluid or ignores how foaming changes at higher speeds. Matching nozzle design, fill timing, and drip control to the way a product actually moves prevents most volume giveaway and cleanup delays before they start. Sealing follows the same logic under line pressure. A cap that torques cleanly at low speed can behave differently when film tension, temperature, and conveyor pace shift during a long run. Rather than chasing perfect settings every shift, plants get more value from recording the narrow ranges that still hold a reliable seal and making those ranges easy to repeat. Standardizing changeover sequences helps here, not by adding paperwork, but by arranging tooling, recipe loading, and adjustment checks in the same physical order so a rushed switch does not quietly skip a critical step.
Inspection often becomes a bottleneck because it is placed where rejected units have nowhere to go except back into the operator's walking path. Putting short rejection lanes, buffering space, or side transfer points directly after the checkweigher or vision system keeps good containers moving while bad ones leave the line without manual handling. Sanitary design also benefits from this practical view. Sloped surfaces, standoff mounts, and accessible drain points matter less as checklist items than as details that shorten washdown and reduce the chance of water pooling in hidden corners. Line layout changes that reduce walking and waiting often outperform software tweaks alone. When operators can see the filler, sealer, and inspection screen from one position, and when supplies are staged within arm's reach, small stoppages get resolved before they turn into downtime records.
Contact Us
Contact Person: Tyson
Email: [email protected]
Tel/WhatsApp: +8613396971296
Website: https://www.wanyingmachinery.com