Window Blinds Factory: How Your Blinds Are Made From Start to Finish
2026-11-16
Ever watched a blind being assembled and thought it’s just a few pieces of plastic? Think again. Inside a real window blinds factory, the process is a mix of precision engineering and hands-on craftsmanship — from cutting the fabric to testing the final lift. At ROLLERGY, we don’t just manufacture blinds; we obsess over every millimeter so your windows get exactly what they deserve. Here’s the full journey, start to finish.
What Happens Before a Blind Is a Blind
Long before a blind hangs in a window, its journey begins with raw materials that rarely look anything like the finished product. Aluminum coils, wooden slats, or fabric rolls arrive at the factory in bulk, often still bearing mill marks or dye lot variations. Workers inspect each batch for warping, color inconsistency, and surface defects, rejecting anything that won't hold up under daily use. Only after this initial screening do the materials move to the cutting floor.
At the cutting stage, precision matters more than speed. Slats are sliced to exact widths, headrails are milled to fit specific window dimensions, and cords are cut to predetermined lengths. Each component is labeled with a job number, so that a slat from one batch never gets mixed with a headrail from another. This is also when any decorative finishes—like embossing or painting—are applied, before the pieces are assembled into a functional blind.
The final pre-assembly step is quality control at the component level. Every cord, tilt mechanism, and end cap is tested in isolation. If a cord frays or a mechanism sticks, it's discarded before it can compromise the whole unit. This piece-by-piece verification is what separates a blind that lasts a decade from one that fails in a season—work that happens quietly, before the blind ever becomes a blind.
Slats, Ladders, and the Geometry of a Clean Cut
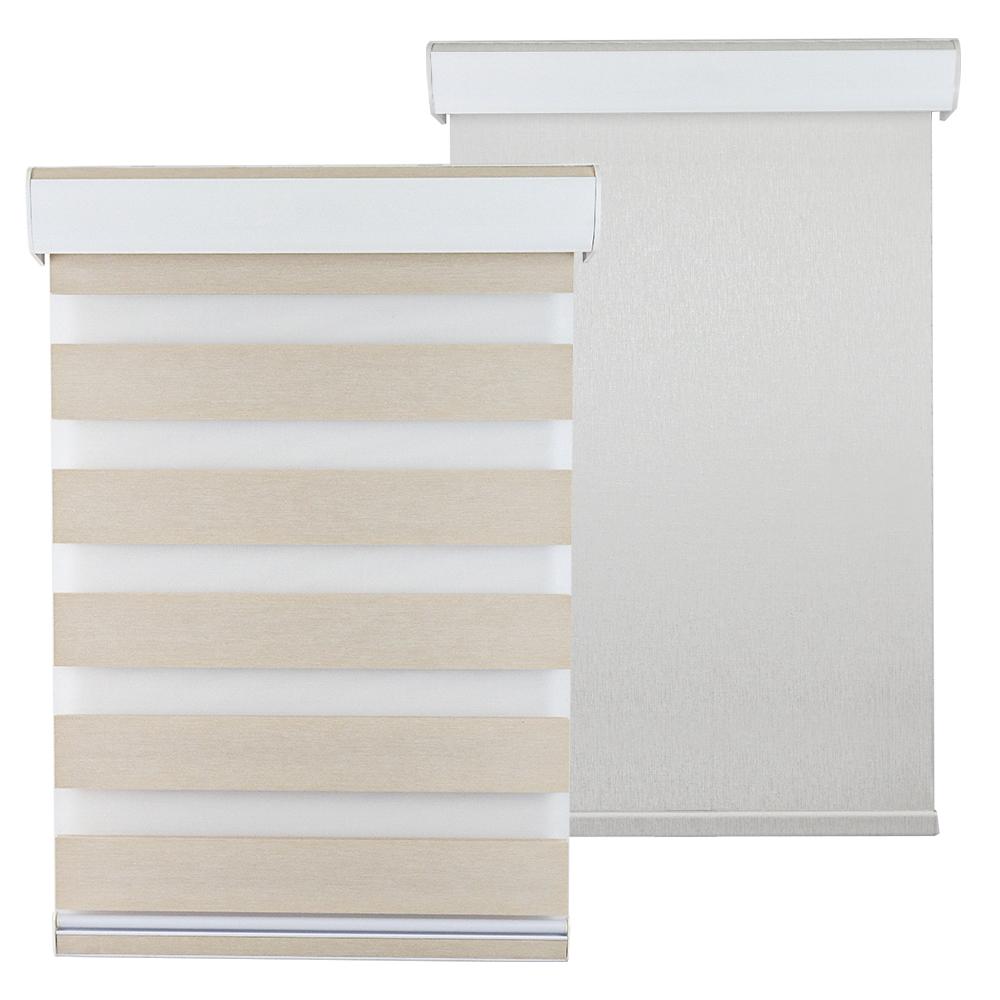
Anyone who has wrestled a circular saw through a sheet of plywood knows that a straight line is never as straight as it looks from the driver's seat. That's where slats and ladders earn their keep. A slat—a thin strip of wood or metal—becomes a physical ruler, guiding the saw's shoe along a path that doesn't waver when your shoulder gets tired. A ladder, or a pair of clamped straightedges, does the same job for longer rips, turning a wobbly freehand cut into something you'd be proud to frame.
The geometry part isn't fancy. It's mostly about parallelism and the fact that a blade's kerf removes material on one side of your pencil mark. If you line up the slat on the wrong side, your finished piece ends up a blade-width short. Experienced hands will tell you to measure from the blade's teeth, not the saw's edge, and to let the slat define the cut rather than your eye. The ladder setup helps when you need repeated, identical strips: set the distance once, then slide the workpiece against a stop block after each pass.
A clean cut is less about brute force and more about controlling the variables—blade sharpness, feed rate, and a guide that doesn't flex. Slats and ladders remove the guesswork from the equation, so the only thing left to watch is the sawdust spraying in a straight line. It's a small victory, but on a Saturday afternoon in the garage, it feels like you've outsmarted the wood itself.
Where Cordless Lifts Get Their Quiet Strength
The low hum that defines a cordless lift isn't an accident. Designers strip away the engine noise and vibration that dominate corded or hydraulic alternatives by pairing a brushless DC motor with a helical gear set. The brushless design eliminates the friction and sparking of traditional brushed motors, while helical gears engage more gradually than straight-cut teeth, cutting down the high-frequency whine that usually signals strain. That combination alone removes most of the mechanical racket before any sound dampening even enters the picture.
But quiet strength also lives in the battery and control system. Lithium-ion packs deliver steady voltage without the sag that makes older lead-acid lifts surge and groan under load. A smart controller meters current in tiny increments, so the motor never has to "grab" for power — it glides through starts and stops. This electronic smoothness translates directly into acoustic calm, and it also protects the frame from the jolts that would otherwise loosen joints and create rattles over time.
Finally, the structure itself acts as a sound manager. Thick, ribbed aluminum extrusions and bonded steel panels push resonant frequencies out of the audible range. Sealed bearings, isolation mounts for the motor, and carefully routed wiring keep metal-on-metal contact to a minimum. The result is a lift that doesn't need to shout about its capacity — the silence under load is proof enough.
Powder Coating's Dirty Little Secret to Lasting Color
Most people assume a vibrant powder-coated finish comes down to the topcoat itself. That’s only half the story. The real anchor for lasting color is what happens before the powder ever touches the metal—specifically, how the substrate is cleaned and pretreated. Skipping a proper phosphate or zirconium conversion coating might save a few minutes on the line, but it quietly invites color fade, chalking, and adhesion failures within the first year of outdoor exposure. The powder can’t do its job if the surface underneath is fighting it.
Another overlooked factor is cure temperature control. Powder coatings are formulated to cross-link within a narrow heat window. Run the oven too cool and the pigment particles never fully lock into the resin matrix—colors look dull and wash out quickly. Run it too hot and the binder degrades, causing yellowing in whites and pastels. Many coaters chase “good enough” readings with a single probe, while hot and cold spots across the part create inconsistent color retention. The dirty secret? A $50 infrared thermometer and a slower line speed often outperform expensive powder on poorly managed ovens.
Finally, UV-stable pigments matter more than gloss level. Cheap organic reds, yellows, and blues can look stunning on day one but break down under sunlight within months. The best shops don’t just pick a color—they ask for accelerated weathering test data and batch-level pigment certification. When you combine a clean conversion-coated surface, precise cure profiling, and UV-resistant pigments, the same powder can look fresh for a decade instead of two summers.
The Inspection Station That Rejects Perfect-Looking Blinds
Most people assume a blind that hangs straight and shows no creases has already passed every reasonable test. But the inspection station here operates on a different principle. It is not enough for a fabric to sit flat, align with the window frame, or photograph well from three feet away. Inspectors slide their fingers along the hem, lift the blind at shallow angles against overhead light, and run a slow tension check along every cord. A panel can look flawless on the surface and still be rejected for a near-invisible stitching drift, a tiny variation in weave tension, or a control mechanism that sounds slightly different from the reference unit.
The station's rejection rate surprises new team members because the rejected pieces rarely look defective. Some simply do not roll at the same speed after a hundred cycles. Others have a micro-gap between slats that a customer would never notice on day one but could widen after repeated use. The inspectors keep a physical sample board of past failures, not as a warning but as a reminder that appearance is only the first gate. A blind that leaves this station has already survived a stricter definition of finished than the one visible from the showroom floor.
Packing a Blind So It Arrives Without a Single Crease
A folded blind almost always arrives with sharp lines pressed into the fabric, especially if it has a blackout or thermal backing. The only reliable way to keep it smooth is to roll it rather than fold it. Lay the blind face down on a clean, dry surface and smooth out any wrinkles with your hands before you start. If the blind has slats or a stiffened header, work from the bottom edge up so the natural curve of the roll doesn't fight the hardware.
Place a length of acid-free tissue paper or a clean cotton sheet over the fabric as you roll. This extra layer stops the face of the blind from rubbing against its own backing and prevents impressions from forming during transit. Roll slowly, keeping the tension even but not tight—too much pressure can leave a spiral mark that's almost impossible to remove. For wider blinds, a second pair of hands helps keep the roll straight and prevents one end from bulging.
Once the blind is rolled, slide it into a rigid mailing tube that gives you at least an inch of clearance on all sides. Fill the empty space at each end with crumpled kraft paper or foam discs so the roll cannot shift if the package is dropped. If you must pack a folding blind and rolling isn't an option, use wide, soft folds with tissue paper tucked inside each bend, but expect to steam it lightly on arrival.
FAQ
Most window blinds start with aluminum, vinyl, wood, or fabric. The factory will often run separate lines for each material because cutting and shaping methods differ quite a bit. You might see huge rolls of vinyl being unrolled in one corner and stacks of basswood slats in another.
After the raw material is inspected, automated saws or shears cut it into slats according to the order’s measurements. For wooden blinds, each slat gets a light sanding on the edges right after cutting so they don’t splinter later during assembly.
Slats travel through a finishing booth where they receive stain, paint, or a protective coating. They’re usually hung or placed on a conveyor so both sides dry evenly, and some factories use heat lamps to speed up the curing process without leaving streaks.
A specialized drilling machine punches or drills holes through each slat at the same position. The pattern has to match the ladder strings and lift cords precisely, or the final blind will hang unevenly and be difficult to operate.
Assembly often happens on long tables with jigs that hold the slats in order. Workers thread the ladder cords through the route holes, attach the headrail, and then feed the lift cords down through the stack. It’s a mix of handwork and small pneumatic tools that keep everything taut.
Yes, many lines are built for made-to-measure orders rather than stock sizes. A technician enters the window dimensions into a computer, and the cutting, drilling, and trimming stations adjust automatically, so odd angles or arched tops get special treatment on separate jigs.
Each blind is raised and lowered a few times on a testing rack, and inspectors check that the slats nest evenly when fully closed. They also run a hand along the edges and inspect the cords for fraying or irregular tension, then wipe the slats clean before wrapping.
Finished blinds get wrapped in thin foam or paper sleeves, then slid into sturdy cardboard boxes with foam end caps to keep the hardware from shifting. Smaller parts like mounting brackets and wand tilters are bagged separately and taped inside so nothing rattles during transit.
Conclusion
Before a single slat is cut, the process starts with raw material checks and precise measurements. The team verifies each width, drop, and control type against the order, ensuring the fabric or wood veneer is free of flaws before it ever touches a cutting table. This early stage sets the tone for everything that follows, because a blind that starts wrong stays wrong no matter how clean the later steps look.
Once the materials pass inspection, the cutting and assembly line takes over. Slats are sliced with angled blades for crisp edges, ladders are spaced to prevent sag, and cordless lift mechanisms are tension-tested to hold their quiet strength. Powder coating gets its durability from a thick, even cure rather than a quick spray, while a final inspection station deliberately rejects pieces that look perfect to the naked eye but fail a tactile or alignment check. Packing wraps everything in padded, crease-free layers, so the blind arrives at your door exactly as it left the factory floor.
Contact Us
Contact Person: Vivien Cheng
Email: [email protected]
Tel/WhatsApp: +86 13751758835
Website: https://www.rollergytech.com/